

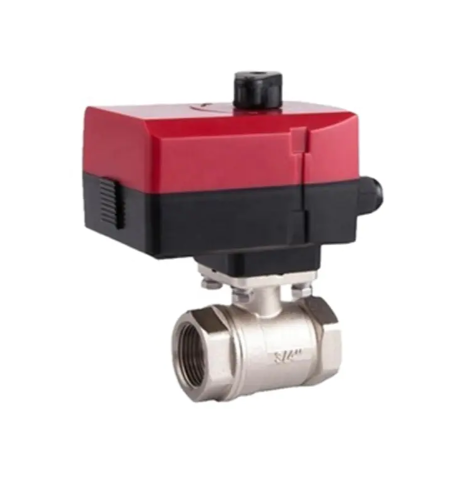
Valves play a vital role in regulating the flow of liquids and gases in industrial systems. A Motorized Valve Manufacturer provides essential components that allow for precise control and automation, helping facilities improve efficiency and safety.
A Motorized Valve Manufacturer typically produces valves equipped with electric actuators, enabling automated operation. These valves are widely used in industries such as water treatment, HVAC, oil and gas, and chemical processing. By integrating a motor, the valve can open, close, or adjust flow without manual intervention, reducing labor requirements and improving system response time.
Quality and reliability are key considerations for a Motorized Valve Manufacturer. High-quality materials such as stainless steel, brass, or durable plastics are commonly used to ensure resistance to corrosion, temperature fluctuations, and pressure variations. The manufacturing process often involves precision machining and strict testing protocols to confirm that each valve meets operational specifications and safety standards.
Customization is another important aspect offered by a Motorized Valve Manufacturer. Clients may require valves with specific pressure ratings, sizes, or actuator configurations. Some manufacturers also offer programmable controls, allowing valves to be integrated into automated systems or monitored remotely. By providing tailored solutions, manufacturers ensure that their valves meet the exact needs of diverse applications.
Testing and quality assurance are critical services provided by a Motorized Valve Manufacturer. Valves are often tested for leakage, torque, response time, and durability under varying conditions. Compliance with international standards such as ISO or IEC ensures that the products are suitable for industrial environments. These procedures provide confidence that the motorized valves will perform reliably over time.
Maintenance and technical support are additional considerations when working with a Motorized Valve Manufacturer. Proper installation, regular inspection, and occasional calibration help maintain performance and extend the valve's lifespan. Many manufacturers provide guidance on troubleshooting, replacement parts, and preventive maintenance to help clients avoid downtime and maintain system efficiency.
Choosing the right Motorized Valve Manufacturer involves evaluating production experience, product range, and customer support. Factories with established track records and verified certifications are more likely to deliver reliable and consistent products. Reviewing technical documentation, requesting samples, or visiting manufacturing facilities can help clients assess quality and compatibility with their systems.
A Motorized Valve Manufacturer also contributes to operational efficiency by providing valves that integrate with automation systems. These valves can be controlled through PLCs or other control units, enabling precise flow management and system optimization. Such integration reduces manual intervention, minimizes errors, and improves overall process control.
A Motorized Valve Manufacturer provides more than just valves; it offers solutions that enhance operational efficiency, safety, and automation in industrial systems. Through careful material selection, precision manufacturing, customization, and quality assurance, these manufacturers deliver products that meet the demands of modern industrial applications. Partnering with a reliable manufacturer ensures consistent performance, reduced downtime, and improved control over fluid systems.

 English
 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Russian
 Romaian
 Portuguese (Brazil)
 Greek