

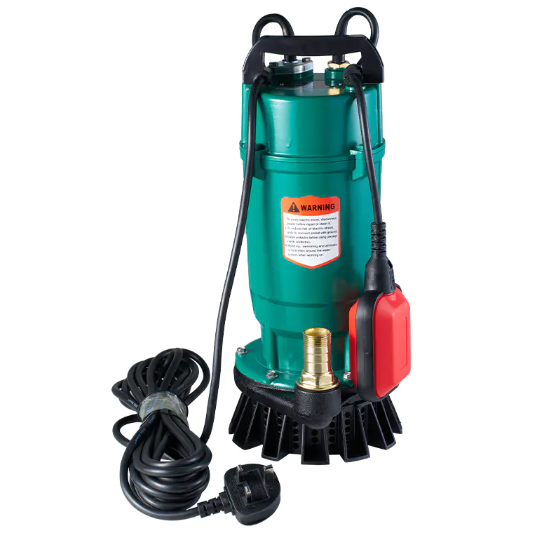
Submersible pumps are widely used in water supply, sewage treatment, irrigation, and industrial applications. Their ability to operate fully submerged in water or other liquids makes them efficient and versatile. The quality and performance of these pumps depend heavily on the expertise and production practices of a submersible pump factory.
A submersible pump factory typically begins with careful material selection. Pumps need corrosion-resistant metals, high-quality seals, and durable electrical components to ensure long-term operation. Stainless steel, bronze, or coated cast iron is often used for pump casings to prevent rust and wear. By combining these materials with precision engineering, a submersible pump factory produces pumps that can function reliably under continuous immersion.
The manufacturing process in a submersible pump factory involves multiple stages, including casting or machining the pump housing, assembling the motor and impeller, and installing seals and wiring. Precision in these steps ensures proper alignment and balance, which reduces vibration, noise, and wear. A well-managed submersible pump factory also implements quality checks at each stage, ensuring consistency and adherence to performance specifications.
Quality control is a major focus for any submersible pump factory. Each pump is tested for flow rate, pressure, electrical insulation, and resistance to leakage. Performance under different water conditions may also be evaluated to ensure reliability. By maintaining strict quality standards, a submersible pump factory provides products that meet industrial, agricultural, and domestic requirements.
Customization is another important aspect offered by many submersible pump factories. Customers can request pumps with specific flow capacities, motor types, or impeller designs to suit particular applications. Some factories also provide options for different voltage ratings, cable lengths, or protective coatings. These customization options make pumps adaptable to diverse operational needs.
Durability and maintenance are key considerations for pumps produced by a submersible pump factory. High-quality seals, bearings, and electrical components reduce wear and minimize downtime. Routine maintenance, including checking for debris, monitoring motor performance, and replacing worn seals, helps extend the pump's service life. Reliable submersible pumps reduce repair costs and improve operational efficiency.
Environmental and safety standards are increasingly important in modern manufacturing. Many submersible pump factories use eco-friendly materials, energy-efficient motors, and compliant insulation to reduce environmental impact and ensure safe operation. Responsible manufacturing practices contribute to sustainability while maintaining product reliability.
Applications of pumps from a reputable submersible pump factory are extensive. They are used in residential water supply, agricultural irrigation, wastewater management, mining operations, and industrial liquid transfer. Choosing a reliable submersible pump factory ensures that products meet safety regulations, provide consistent performance, and suit a variety of applications.
A submersible pump factory plays a crucial role in producing durable, reliable, and customizable pumps for multiple sectors. By focusing on material quality, precise manufacturing, rigorous testing, and adaptable design, these factories ensure that pumps deliver consistent performance. Selecting products from a trusted submersible pump factory provides confidence in both efficiency and long-term reliability.

 English
 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Russian
 Romaian
 Portuguese (Brazil)
 Greek