

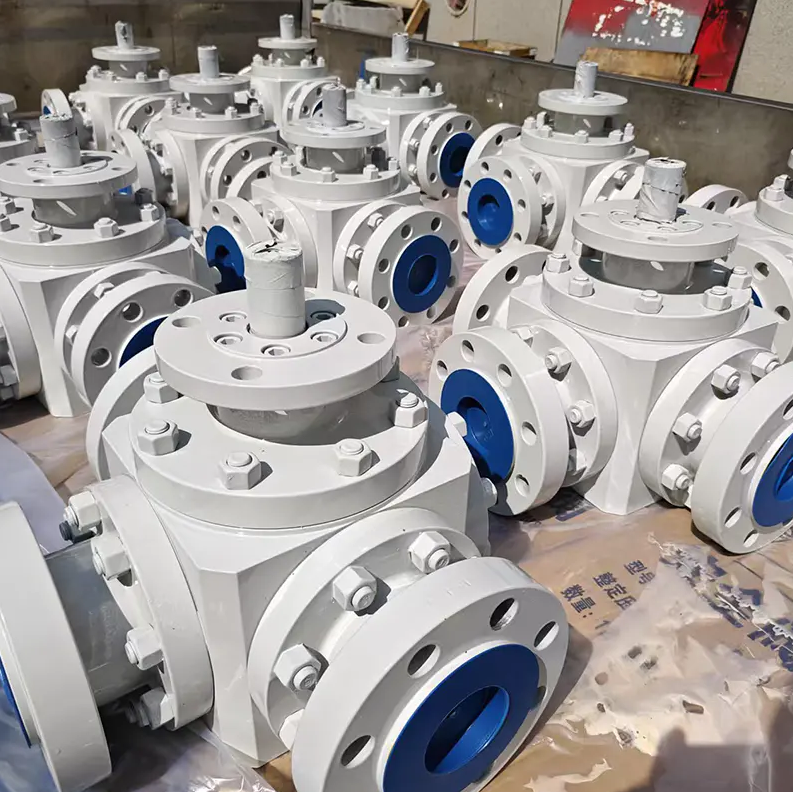
Floating ball valves are widely used in industrial, commercial, and residential applications due to their simple design and reliable operation. The performance and durability of these valves depend heavily on the expertise of a Floating Ball Valve Manufacturer, who focuses on quality materials, precise engineering, and thorough testing to meet a range of operational requirements.
A Floating Ball Valve Manufacturer typically starts by selecting high-quality materials for both the ball and the valve body. Stainless steel, brass, and carbon steel are common choices, chosen for their resistance to corrosion, wear, and high-pressure conditions. The quality of these materials directly influences the valve's ability to maintain a tight seal and operate reliably over time.
The production process in a Floating Ball Valve Manufacturer involves several critical steps. The ball is machined to precise dimensions to ensure smooth rotation and tight sealing with the valve seats. The valve body is fabricated and finished to withstand internal pressure and environmental conditions. Proper alignment and assembly of all components are essential to guarantee leak-free operation and consistent performance.
Testing and quality control are fundamental to a Floating Ball Valve Manufacturer's operations. Valves undergo pressure testing, leakage assessment, and functional inspections to verify that they meet specified standards. These evaluations ensure that the valves can handle different fluid types, pressures, and temperatures without compromising safety or efficiency.
Customization is another feature offered by a Floating Ball Valve Manufacturer. Clients may request valves with specific sizes, pressure ratings, or end connections to meet the needs of their particular systems. Some manufacturers also provide options for fire-safe designs, anti-static devices, or special coatings to improve chemical resistance. This flexibility allows industries to obtain valves that are suitable for their exact applications.
Durability is a key consideration for a Floating Ball Valve Manufacturer. By using corrosion-resistant materials and precision engineering, the valves can withstand long-term exposure to liquids, gases, and varying temperatures. Properly constructed floating ball valves reduce maintenance frequency, prevent unexpected downtime, and extend service life in industrial systems.
Safety is another priority for a Floating Ball Valve Manufacturer. Proper sealing, reliable materials, and rigorous testing help prevent leakage and failures, which is essential in high-pressure or hazardous fluid applications. Valves are designed to operate smoothly and securely, minimizing risks for both equipment and operators.
Technical support is often provided by a Floating Ball Valve Manufacturer to help clients select the right valve and integrate it effectively into their systems. Guidance on installation, operation, and maintenance ensures that valves perform as expected and meet safety standards over time.
A Floating Ball Valve Manufacturer plays a critical role in producing durable, reliable, and efficient valves for various industries. Through careful material selection, precise manufacturing, thorough testing, and client support, these manufacturers ensure that floating ball valves perform consistently and safely. Their expertise enables users to implement valves that provide dependable flow control and long-term operational reliability.

 English
 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Russian
 Romaian
 Portuguese (Brazil)
 Greek